
14 Şubat Alüminyum Gaz Giderme Yöntemleri
Aluminum degassing removes dissolved hydrogen from molten aluminum before casting, helping reduce the risk of hydrogen-related porosity in the finished product. The main industrial methods include gas purging through a static lance and rotary impeller degassing, which disperses inert gas into smaller bubbles. For continuous aluminum casting lines, an online degassing unit integrates rotary treatment into the metal transfer process. The appropriate method depends on the required melt quality, metal throughput, alloy, and production conditions.
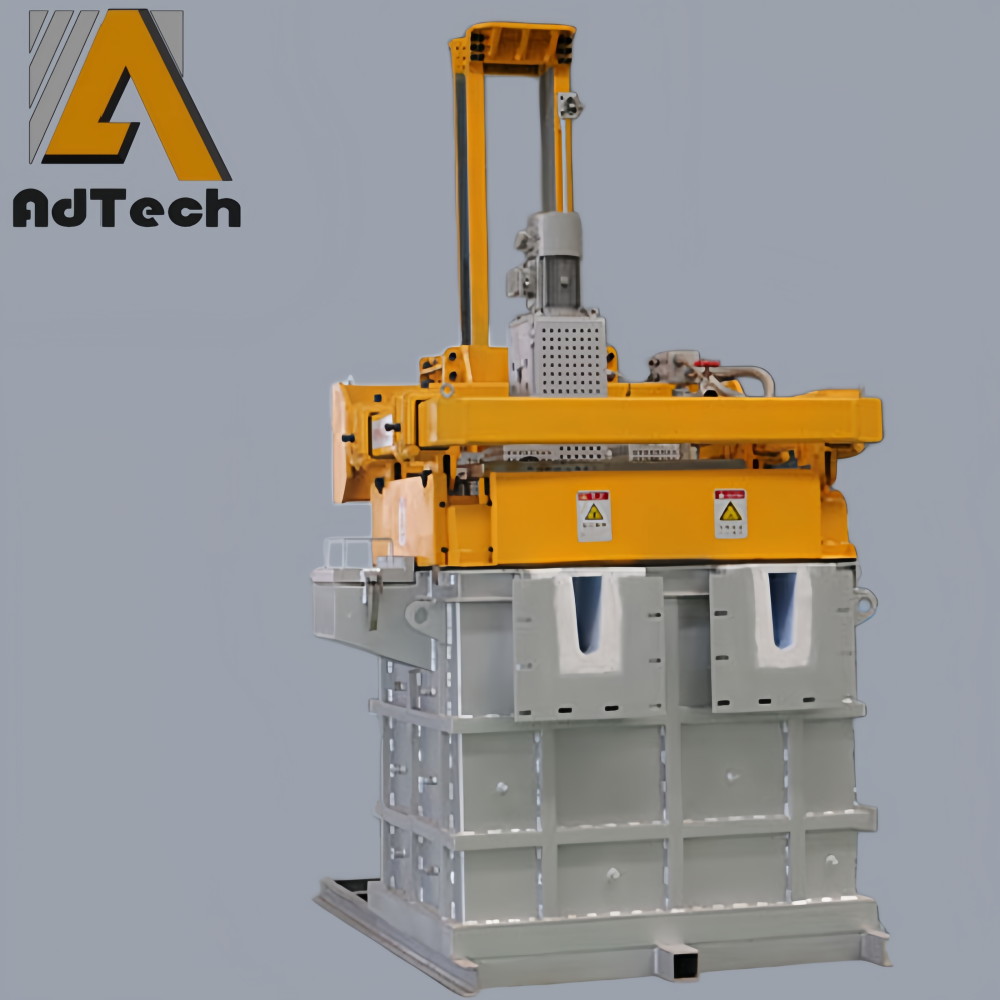
Gaz giderme ekipmanı
Why Does Molten Aluminum Need Degassing?
Hydrogen is the principal gas responsible for gas porosity in aluminum castings. It dissolves in liquid aluminum, but its solubility decreases sharply as the metal solidifies. If the remaining liquid cannot release hydrogen quickly enough, gas pores may develop within the casting.
Hydrogen pickup occurs primarily through reactions involving moisture. Atmospheric water vapor can react at the molten metal surface, introducing hydrogen into the melt. Wet charge materials, inadequately dried tools, and moisture-contaminated additions can create similar problems.
Hydrogen-related porosity must be distinguished from non-metallic inclusions. Both can affect casting quality, but they require different treatment strategies: degassing primarily targets dissolved hydrogen, while filtration primarily removes solid particles and oxide-related inclusions.
| Contamination source | How it affects molten aluminum | Relevant control measure |
|---|---|---|
| Atmospheric humidity | Water vapor can react at the melt surface and introduce hydrogen | Limit unnecessary melt exposure and turbulence |
| Wet charge materials | Moisture can react with molten aluminum | Ensure appropriate drying and charge preparation |
| Wet tools and equipment | Residual moisture can introduce hydrogen during contact with hot metal | Use suitable preheating and drying procedures |
| Contaminated gas supply | Moisture in purge gas or gas lines can undermine treatment | Verify gas quality and supply-system condition |
| Excessive melt disturbance | Can promote oxidation and entrainment of oxide films | Maintain controlled gas flow and rotor operation |
The aim of degassing is to reduce hydrogen before the metal reaches the casting stage. However, the result depends on the initial hydrogen concentration, gas dispersion, treatment time, melt temperature, and process control.
What Are the Main Aluminum Degassing Methods?
Static lance degassing and rotary impeller degassing both introduce purge gas into molten aluminum, but they differ in how the gas is dispersed.
An online degassing unit is an equipment configuration that commonly uses rotary degassing within a dedicated treatment chamber installed between the furnace and casting equipment.
| Yöntem | Gas dispersion | Main advantages | Key limitations |
|---|---|---|---|
| Static lance degassing | Gas enters through a submerged lance, often forming relatively large bubbles unless a suitable diffuser is used | Simple equipment and relatively low initial investment | Coarser bubble dispersion may limit gas-metal contact |
| Rotary impeller degassing | A rotating rotor breaks the injected gas into smaller, dispersed bubbles | Greater gas-metal interfacial area and more controlled bubble distribution | Requires control of rotor speed, gas flow, and treatment time |
| Çevrimiçi gaz giderme ünitesi | Rotary treatment integrated into a continuous or controlled metal-transfer system | Integrates hydrogen removal with production-line operation; may include temperature control | Requires equipment sizing, installation coordination, and operating control |
These methods should not be ranked solely by equipment cost. A static lance may be adequate for some applications, while demanding casting operations may benefit from the more controlled gas dispersion of rotary treatment. An online degassing unit is particularly relevant when melt treatment must be incorporated into the normal production flow.
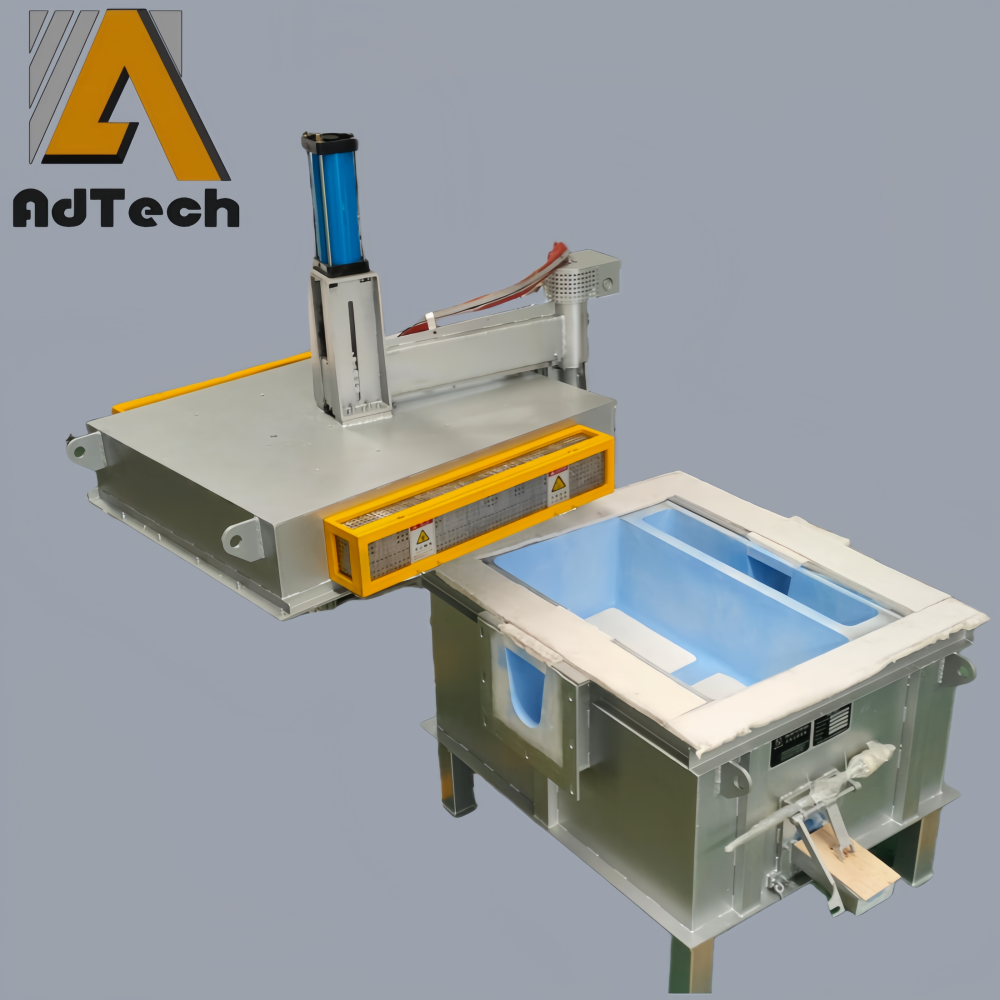
e-heating Plaka Tipi Filtre Ekipmanı
How Does Static Lance Degassing Work?
Static lance degassing introduces nitrogen, argon, or another specified purge gas through a submerged lance. The gas rises through the liquid aluminum, and dissolved hydrogen transfers from the melt into the bubbles before being carried toward the surface.
The simplicity of the lance arrangement can make it attractive for certain batch-treatment applications. However, its performance depends on the lance design, gas flow, immersion depth, bubble size, treatment duration, and melt volume.
Large bubbles generally provide less gas-metal interfacial area per unit volume of gas than smaller bubbles. This can limit hydrogen transfer when the gas is poorly dispersed.
Another consideration is surface disturbance. Excessive bubbling at the melt surface can promote oxidation and introduce additional oxide films. It is therefore inaccurate to assume that increasing gas flow will always improve degassing.
Static lance treatment should be evaluated against measured hydrogen levels and the quality requirements of the casting process rather than judged by the visible intensity of bubbling.
Why Is Rotary Impeller Degassing Widely Used?
Rotary degassing introduces purge gas through a rotating shaft and rotor immersed in molten aluminum. The rotor disperses the gas into smaller bubbles and distributes them through the melt.
Because smaller bubbles provide a larger total interfacial area for the same gas volume, they can support more effective hydrogen transfer when the process is properly controlled.
The mechanism involves hydrogen diffusion from the liquid aluminum into the bubbles. The bubbles then rise and release the collected gas at the melt surface. Depending on the process conditions, some solid inclusions may also attach to bubbles or accumulate in the surface layer, but this does not make rotary degassing a substitute for dedicated filtration.
A rotary degassing system must be operated within a suitable process window.
| Operating parameter | Effect on degassing | What needs to be controlled |
|---|---|---|
| Rotor speed | Influences bubble breakup and melt circulation | Avoid inadequate dispersion and excessive turbulence |
| Gas flow rate | Determines the amount of purge gas introduced | Match flow to rotor design and treatment requirements |
| Treatment time | Affects hydrogen removal | Confirm effectiveness through melt-quality measurements |
| Rotor geometry | Influences bubble distribution and circulation | Select a rotor suitable for the equipment and alloy |
| Melt temperature | Affects hydrogen behavior and process conditions | Follow the alloy and equipment operating specification |
| Initial hydrogen level | Influences the required treatment effort | Measure the melt where practical |
| Gas purity | Affects treatment reliability and contamination risk | Maintain appropriate gas and pipeline quality |
Rotary degassing performance is therefore determined by the combined effect of gas flow, rotor behavior, treatment time, and melt conditions rather than by one operating parameter alone.
Research published in Metallurgical and Materials Transactions B has also shown that purge-gas selection can affect oxide- and nitride-film populations in aluminum melts. Nitrogen and argon should therefore not be treated as universally interchangeable for every alloy and cleanliness requirement.
Should You Use Nitrogen or Argon for Aluminum Degassing?
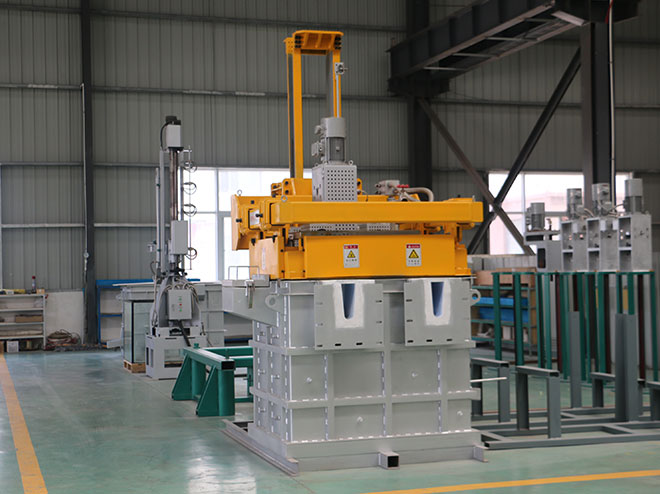
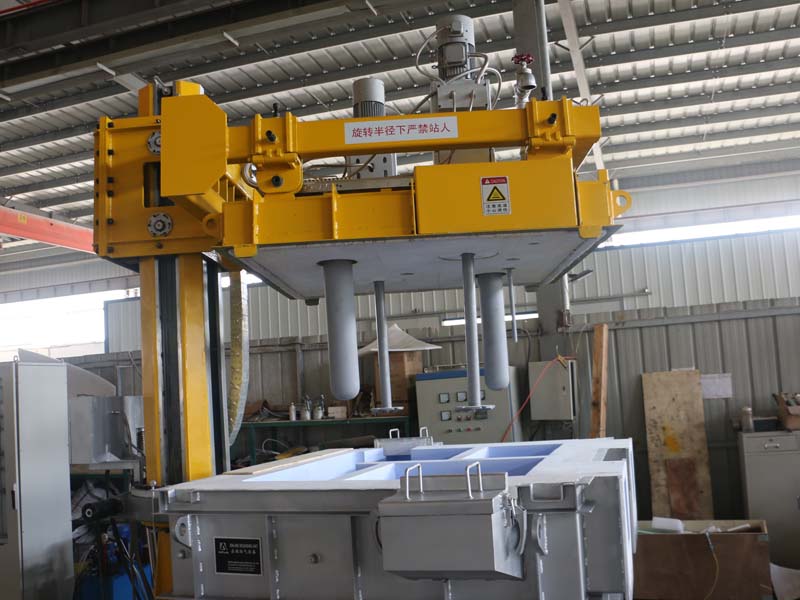
Adtech online degassing equipment
Nitrogen and argon are both used in aluminum melt treatment, but the appropriate choice depends on alloy composition, product requirements, gas cost, and the process specification.
Nitrogen is often selected for its availability and lower cost. Argon is highly inert and may be preferred where the alloy, process conditions, or melt-quality requirements justify it.
However, gas selection should not be reduced to a simple rule that nitrogen is always sufficient or argon is always superior. The effects of the purge gas on melt quality depend on the alloy and treatment conditions, including the potential for nitride formation.
| Seçim faktörü | Azot | Argon |
|---|---|---|
| Availability and cost | Often more economical and readily available | Commonly more expensive |
| Chemical behavior | May react with aluminum under certain high-temperature conditions | Highly inert under normal aluminum degassing conditions |
| Application suitability | Widely used when supported by the process specification | Considered where inertness and melt-quality requirements justify its use |
| Final selection | Based on alloy, operating conditions, and quality targets | Based on alloy, operating conditions, and quality targets |
The choice should be confirmed through the relevant equipment specification and melt-quality requirements. Where critical applications are involved, hydrogen measurements and suitable inclusion assessments are more reliable than assuming a particular gas will automatically provide better results.
What Is an Online Degassing Unit?
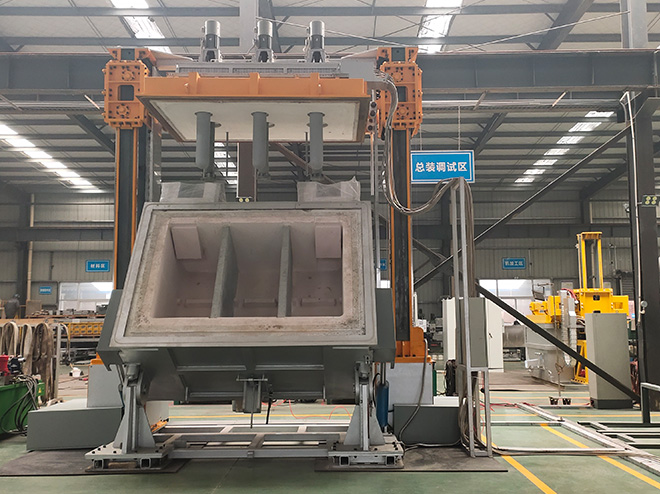
An online degassing unit is installed in the molten aluminum transfer route, typically between the holding furnace and casting equipment. It treats metal as part of the production process, rather than requiring all degassing to be performed as a separate batch operation.
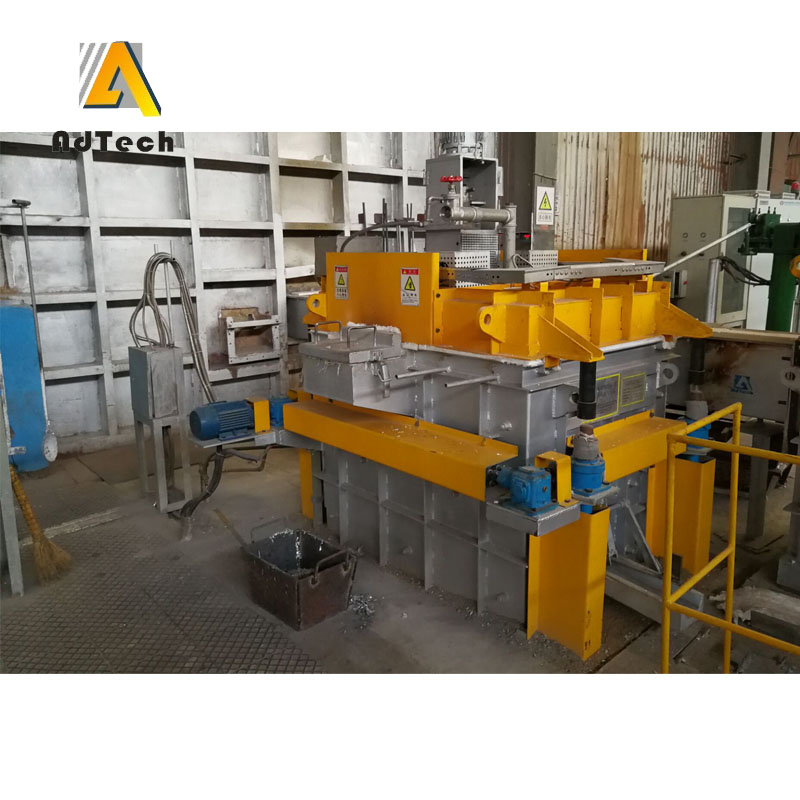
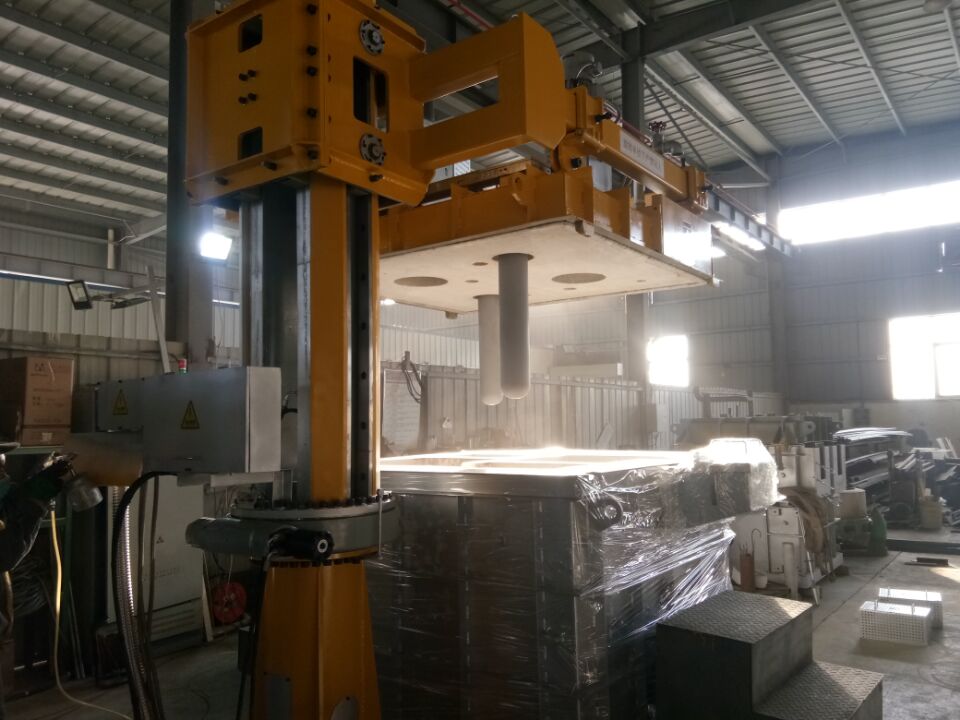
AdTech’in çevrimiçi gaz giderme ünitesi combines a treatment chamber, rotor drive, gas delivery system, and associated components. Depending on the configuration, the equipment can also incorporate electric heating, temperature monitoring, and control functions to help maintain suitable process conditions.
The treatment chamber provides a controlled environment in which purge gas is dispersed through molten aluminum. Its design also needs to accommodate metal inlet and outlet connections, slag management, and access for maintenance.
Metal Degassing Equipment
Key configuration considerations include:
- Required metal throughput and casting-line operating schedule.
- Number of treatment chambers and rotors.
- Gas supply, rotor-speed control, and relevant operating parameters.
- Temperature monitoring and any required heating or holding functions.
- Lining material, rotor compatibility, and replacement access.
- Connections to the upstream launder and downstream filtration equipment.
For continuous casting operations, the unit must be sized and configured to meet the actual production requirements. The appropriate capacity cannot be selected from the final product name alone; alloy, metal flow, casting speed, and target hydrogen level all matter.
How Should an Online Degassing Unit Be Operated?
Operating procedures must follow the equipment manufacturer’s instructions, the alloy requirements, and the plant’s safety procedures. General operating principles can help explain the process, but exact temperatures, gas flow rates, and rotor speeds should not be copied from an unrelated installation.
A typical operating sequence includes:
| Stage | Main action | Amaç |
|---|---|---|
| Preheating | Bring the treatment chamber and relevant components to the specified condition | Reduce thermal shock and avoid introducing an unsuitable cold surface |
| Pre-start inspection | Check connections, seals, rotor condition, gas supply, and safety systems | Confirm readiness for operation |
| Metal introduction | Introduce molten aluminum according to the approved procedure | Establish the required operating metal level |
| Gaz Giderme | Set gas flow and rotor operation according to the process specification | Çözünmüş hidrojen miktarını azaltın |
| Process monitoring | Monitor temperature, flow, rotor operation, and other designated parameters | Maintain stable operating conditions |
| Shutdown or holding | Follow the approved gas, temperature, and restart procedures | Protect the equipment and reduce operational risks |
The operating temperature is alloy- and process-dependent. A temperature such as 780°C should not be treated as a universal startup or production requirement for all aluminum alloys. Excessive temperature can increase energy consumption and may aggravate oxidation or other melt-quality problems.
Hydrogen measurement before and after treatment can help verify effectiveness. Operators should also inspect the rotor, lining, seals, and heating components according to the maintenance schedule.
Does Degassing Also Remove Slag and Inclusions?
Rotary degassing can help bring some inclusions toward the melt surface under suitable conditions, but its principal purpose is the removal of dissolved hydrogen. The extent of secondary inclusion removal varies with the process and should not be assumed to meet every cleanliness target.
Ceramic foam filtration provides a dedicated physical barrier for solid non-metallic inclusions. When both hydrogen and inclusion control are required, degassing and filtration are often used as complementary processes.
| Melt-quality issue | Primary treatment | Important distinction |
|---|---|---|
| Dissolved hydrogen | Gaz Giderme | Reduces dissolved gas content |
| Solid non-metallic inclusions | Seramik köpük filtreleme | Retains particles as metal passes through the filter |
| Surface slag and dross | Suitable skimming and melt-handling procedures | Surface material must be removed appropriately |
| Off-specification dissolved alloy elements | Alloy chemistry management and suitable refining where applicable | Standard degassing does not remove all dissolved metallic impurities |
For integrated casting lines, the placement of the seramik köpük filtre should be coordinated with the degassing unit and transfer system. This helps ensure that hydrogen removal and inclusion filtration are addressed as separate but complementary stages.
How Do You Choose the Right Aluminum Degassing Method?
The correct method depends on the production scale, required hydrogen level, casting process, equipment layout, and available operating resources.
Static lance degassing may suit certain applications where a relatively simple treatment arrangement is adequate. Rotary impeller degassing provides more controlled bubble dispersion and is widely used for molten aluminum treatment. An online degassing unit is suitable when hydrogen removal must be integrated into a casting line with defined throughput and process controls.
For equipment selection, establish the alloy specification, production rate, target hydrogen level, gas supply, installation layout, and downstream filtration requirements before choosing a system.
AdTech supplies online degassing units for aluminum melt treatment, with configurations that can be evaluated against different production capacities and process needs. The appropriate system should be selected based on verified operating requirements, rather than a fixed claim about efficiency or a universal temperature setting.
Reliable aluminum degassing comes from combining suitable equipment, controlled process parameters, clean melt handling, and measurable quality verification. The objective is not simply to generate bubbles, but to reduce dissolved hydrogen while preserving the cleanliness and stability of the molten aluminum delivered to casting.
Sık Sorulan Sorular
1. What are the main methods of aluminum degassing?
The main methods include static lance degassing, rotary impeller degassing, and online degassing using integrated equipment. The appropriate method depends on the casting process, required melt quality, and production capacity.
2. What is the difference between static lance and rotary degassing?
Static lance degassing introduces purge gas through a submerged pipe, while rotary degassing uses a rotating rotor to disperse the gas into smaller bubbles. Rotary degassing generally provides greater gas-metal interfacial area and more controlled bubble dispersion.
3. What gas is used for aluminum degassing?
Nitrogen and argon are commonly used. The choice depends on alloy composition, process requirements, gas purity, and operating cost. Nitrogen should not automatically be considered suitable for every alloy or application.
4. What is an online degassing unit?
An online degassing unit is installed in the molten aluminum transfer route, typically between the holding furnace and casting equipment. It removes dissolved hydrogen as part of the production process.
5. Why does molten aluminum need degassing?
Molten aluminum dissolves hydrogen, but hydrogen solubility decreases during solidification. Excess hydrogen can contribute to gas porosity, which may reduce the quality and performance of cast products.
6. What causes hydrogen to enter molten aluminum?
Moisture is a major source. Atmospheric humidity, wet charge materials, inadequately dried tools, and contaminated additions can introduce hydrogen into the melt.
7. Does rotary degassing remove oxide inclusions?
Its primary function is hydrogen removal. Rotary treatment may assist with the flotation of some inclusions, but ceramic foam filtration is generally used when dedicated removal of solid non-metallic inclusions is required.
8. How can aluminum degassing efficiency be checked?
Hydrogen concentration can be measured before and after treatment using a suitable hydrogen analyzer. Gas flow, rotor speed, treatment time, and melt temperature should also be monitored to help maintain consistent operation.
9. What factors affect the performance of an aluminum degassing unit?
Important factors include rotor design, rotational speed, purge gas flow rate, treatment time, melt temperature, initial hydrogen concentration, and the condition of the gas supply.
10. How do I choose an online degassing unit for my casting line?
Consider the alloy, required metal throughput, target hydrogen level, casting process, available installation space, gas supply, and connection to downstream filtration equipment. These details help determine the appropriate equipment configuration.
İlgili yazılar:
 Alüminyum Gaz Giderme Yöntemleri
 Alüminyum Sıvı Gaz Giderme Sistemi
 Alüminyum Gaz Giderme Yöntemleri
 Alüminyum Gaz Giderme Süreci
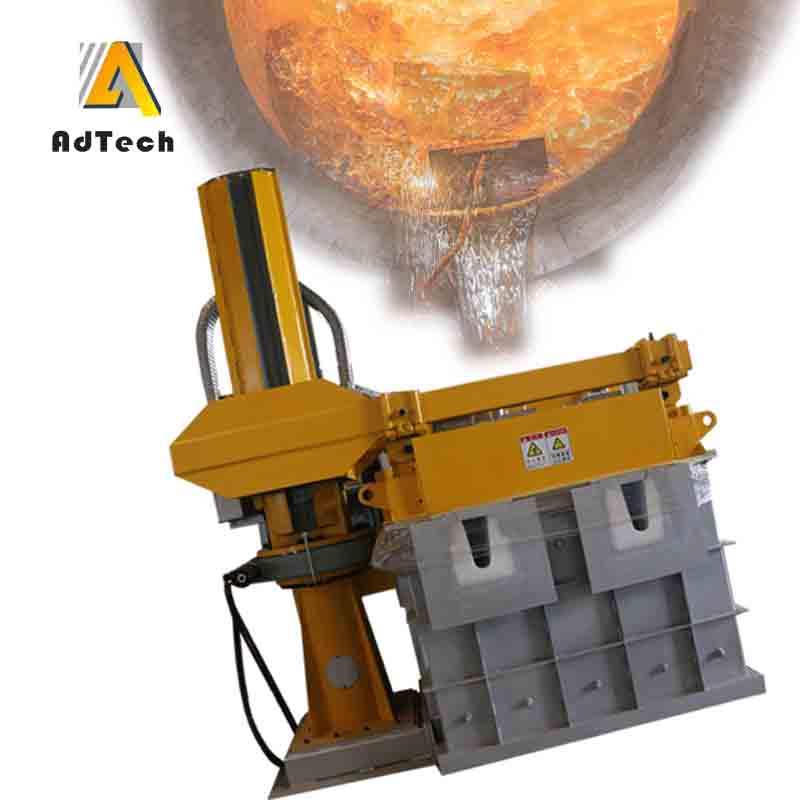 Alüminyumdan Gazın Giderilmesi
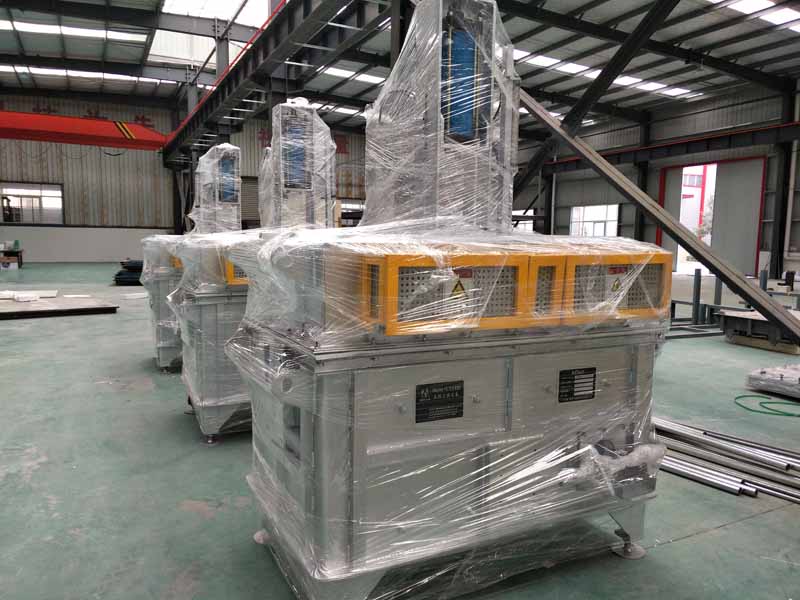 Döner Gaz Giderme Makineleri
 Gaz Giderme Süreci
 Çift Rotorlu Gaz Giderme Ekipmanı
 Alüminyum Dökümde Gaz Giderme
Yüksek Saflıkta Alüminyum için Çevrimiçi Gaz Giderme Ünitesi
 Alüminyum Gaz Giderme Ekipmanı
 Alüminyum Döküm Gaz Giderme Ünitesi
 Alüminyum Hidrojen Gaz Giderme Ekipmanı
 Gaz Giderme Ünitesi
No Comments